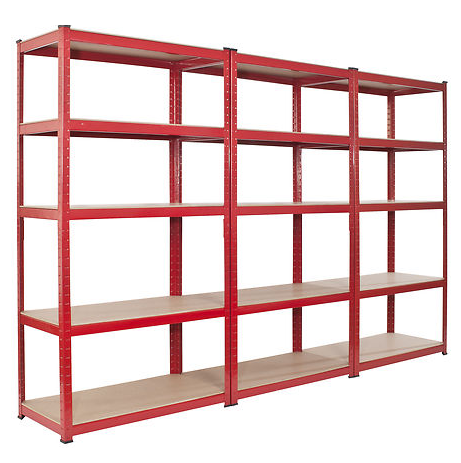
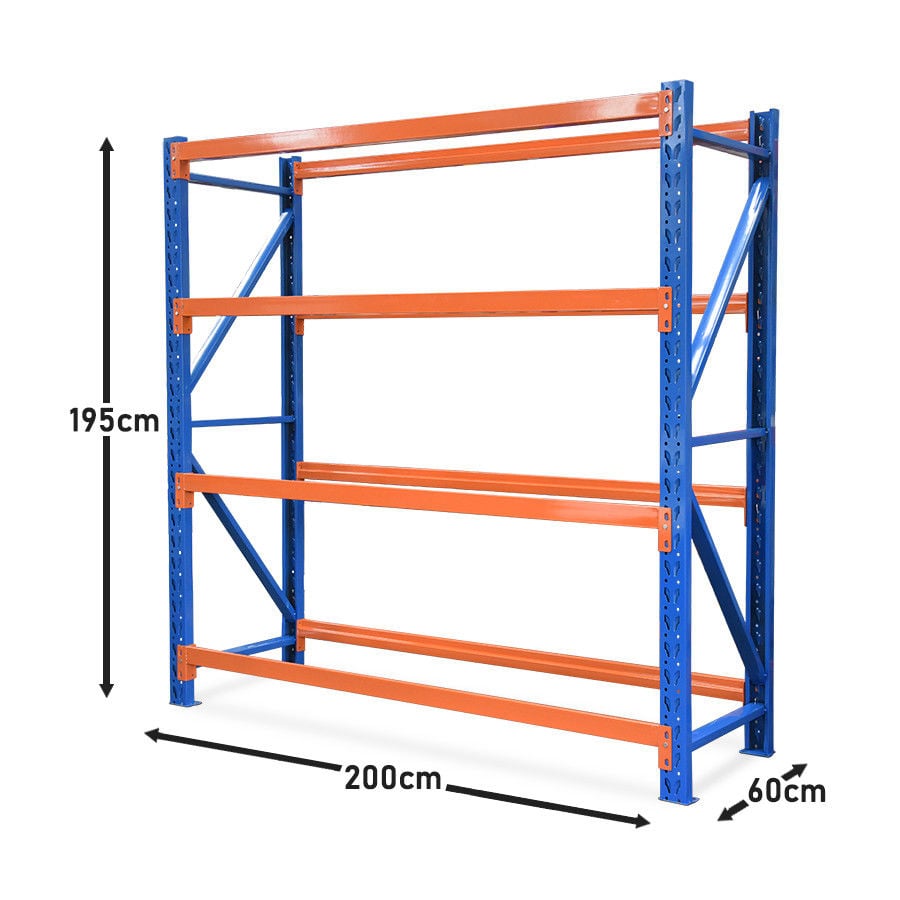
storage shelves factory
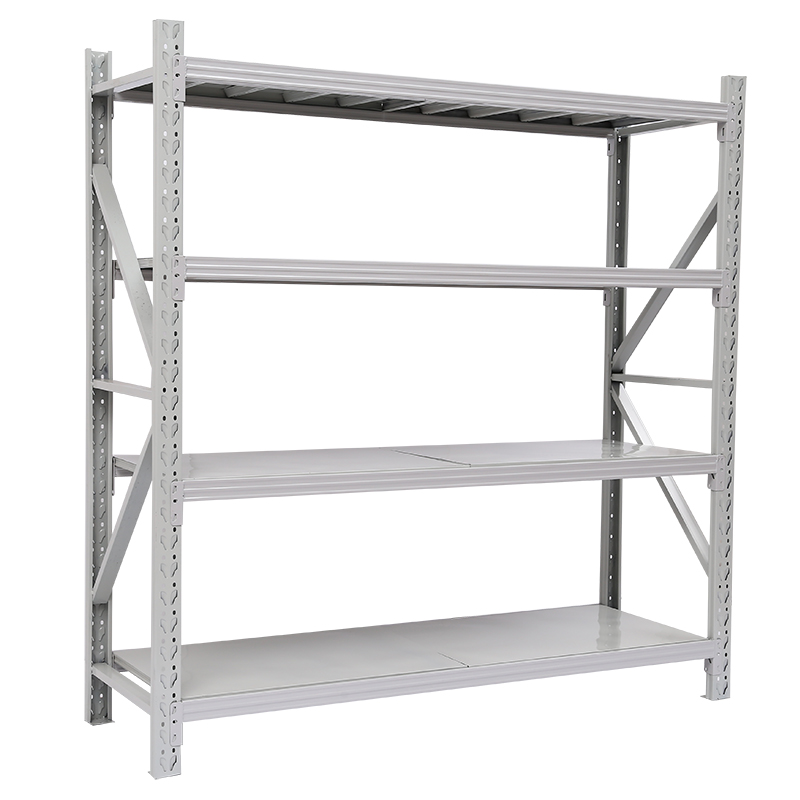
A storage shelves factory represents a specialized manufacturing facility dedicated to producing comprehensive storage solutions for warehouses, retail spaces, industrial facilities, and commercial environments. These factories combine advanced engineering principles with modern production techniques to create durable, versatile shelving systems that maximize space utilization and improve organizational efficiency. The primary function of a storage shelves factory involves designing, fabricating, and distributing various types of shelving units including pallet racking systems, cantilever racks, mezzanine platforms, mobile shelving, and modular storage configurations. Through sophisticated manufacturing processes, these facilities transform raw materials such as cold-rolled steel, stainless steel, and reinforced aluminum into robust storage frameworks capable of supporting substantial weight loads. The technological features integrated within modern storage shelves factory operations include computer-aided design systems, automated cutting and bending machinery, precision welding equipment, powder coating lines, and quality control testing apparatus. These technologies ensure consistent product quality, dimensional accuracy, and structural integrity across all manufactured units. Applications for products from a storage shelves factory span numerous industries including logistics and distribution centers, automotive parts warehousing, pharmaceutical storage, food and beverage facilities, retail merchandising, library systems, and archive management. The factory's production capabilities accommodate custom specifications, allowing clients to order shelving solutions tailored to their unique spatial constraints, load requirements, and operational workflows. Beyond basic manufacturing, a storage shelves factory typically provides comprehensive services including site assessment, load calculation analysis, installation guidance, and after-sales support. This holistic approach ensures customers receive not merely products but complete storage solutions optimized for their specific needs, resulting in improved inventory management, enhanced workplace safety, and maximized return on investment in storage infrastructure.
 EN